Plasma cutting
Compressor for plasma cutting
Screw compressor for plasma cutting, CNC table or hand-held cutter: flow set by the torch, dry filtered air to spare nozzle and electrode. 2-year warranty.
In air plasma cutting, compressed air is not an auxiliary supply: it is the cutting gas. It flows through the torch, is ionised in the arc, blows molten metal out of the kerf and cools the nozzle and electrode on the way. On a hand-held cutter as on a CNC plasma table, cut quality therefore depends directly on the air: enough flow, stable pressure, and dry, filtered air. On a table, air often also drives the zoned fume extraction dampers and the pneumatic marker.
How much air does a plasma cutter need?
The figure that counts is the one from your torch or power source manufacturer: a flow in l/min at a given inlet pressure. It depends on the amperage and the consumables fitted; gouging generally uses more air than cutting. As an indication, typical orders of magnitude are:
- 40 to 45 A hand-held cutter: about 100 to 150 l/min;
- 65 to 105 A power source: about 180 to 220 l/min;
- 125 A power source: about 250 to 280 l/min;
- required inlet pressure: often around 6 to 8 bar.
A typical shop: a CNC table with a 125 A power source (260 l/min), a 45 A hand-held cutter (140 l/min) and a 200 l/min blow gun used now and then, counted at half. That makes 260 + 140 + 100 = 500 l/min. With a 30% margin, you need about 650 l/min, or 0.65 m³/min. Data sheets often give flow in CFM or scfh: our flow and pressure converter does the conversion.
A CNC table cuts for hours on end: that is continuous duty, exactly what a screw compressor is built for.
What pressure does a plasma cutter need?
The power source has its own regulator. It needs a supply pressure slightly above its working pressure, and it must hold it throughout the cut at full flow. If it drops, the arc becomes unstable, the cut bevels and dross appears. A compressor set at around 8 bar is enough in the vast majority of cases. Pressure drops usually come from a hose that is too long or too narrow, or from undersized quick couplings. Check the pressure on the power source gauge during a cut, not at rest.
Which compressor for plasma cutting?
- Hand-held cutter or small table: the K 75, a 7.5 kW 4-in-1 screw compressor, delivers 1.1 m³/min at 8 bar. The 420 L receiver, refrigerated dryer and filtration are built in, so the air leaves the frame dry.
- High-amperage table, or a table plus several hand-held cutters: the K 110 (1.7 m³/min at 8 bar) or the K 150 (2.2 m³/min at 8 bar), both 4-in-1.
- Shop that already has its air treatment: the standalone compressors of the S series, such as the S 150, paired with a dryer sized for their flow.
- Plasma and laser in the same shop: air-assisted laser cutting can need up to 16 bar and even cleaner air. If you have or plan a laser machine, the L series combines a 16 bar compressor, 16 bar receiver, dryer and precision filtration. For plasma alone, 16 bar adds nothing and costs electricity. See compressor for laser cutting.
What air quality for plasma cutting?
Water is plasma's first enemy. Wet air sharply shortens electrode and nozzle life, makes the arc unstable and spoils the cut. Oil and particles disturb the arc too. Good practice:
- A refrigerated dryer after the compressor. It is built into the K series.
- Filtration for particles and oil aerosols. Our compressors are oil-lubricated, so it is the downstream filtration that captures carried-over oil.
- A filter at the power source, in addition to its built-in one, if the manufacturer recommends it.
- No lubricator on the plasma line, and no hose that has carried oiled air.
- Take-offs from the top of the main line, and drains at the low points.
If the torch manufacturer states an air quality class, agree the treatment with our technicians using our ISO 8573-1 guide. See also which air dryer to choose.
Installation and maintenance
- The room. Plasma cutting gives off fumes and very fine metal dust. Install the compressor well away from the table, in a ventilated room with a clean air intake.
- Condensate. An automatic condensate drain on the receiver and at the network low points keeps draining regular. Condensate contains oil: collect it and have it treated.
- Servicing. First service at 500 hours, then every 1,500 hours, with a reminder on the controller. Service kits group the filters and wear parts for each model, and the screw compressor maintenance guide explains each step. 2-year warranty, parts available for 15 years.
To choose your model, use the configurator, estimate the receiver volume with the air receiver size calculator, or send us your power source data sheet with a quote request.
Frequently asked questions — Plasma cutting
Which compressor do I need for a plasma cutter?
Start from the flow and pressure given by your power source manufacturer, add the shop's other uses and a margin of about 30%. For a hand-held cutter or a small table, a 4-in-1 screw compressor such as the K 75 (1.1 m³/min at 8 bar, dryer and filtration built in) is usually suitable. For a high-amperage table or several stations, the K 110 or K 150 take over.
What flow and pressure does plasma cutting need?
The reference is the torch manufacturer's data sheet. As an indication, a 40 to 45 A cutter needs roughly 100 to 150 l/min and a 125 A power source roughly 250 to 280 l/min, with an inlet pressure often between 6 and 8 bar. That pressure must hold during the cut at full flow, not just at rest.
Why do my plasma electrodes and nozzles wear out so fast?
The most common cause is wet or oily air. Water sharply shortens consumable life and makes the arc unstable. Check the dryer, drains and filters, make sure no lubricator is fitted on the line, and measure the pressure at the power source during a cut: pressure that is too low also wears consumables.
Do I need a 16 bar compressor for plasma cutting?
No. Air plasma cutting works with the pressure of a workshop compressor set at around 8 bar. 16 bar is for air-assisted laser cutting: the L series only makes sense if the shop has or plans a laser machine. For plasma alone, higher pressure costs electricity without improving the cut.
Can I connect a plasma cutter to the workshop air network?
Yes, if the network air is dried and filtered. Take the supply from the top of the main line, fit a drain at the low points and add a filter at the power source if the manufacturer recommends it. Avoid any lubricator on that line and use a hose large enough not to lose pressure.
Piston or screw compressor for a 45 A plasma cutter?
A 45 A cutter needs around 100 to 150 l/min at 6 to 8 bar, as a guide: flow is not the issue, dry air and a pressure that holds during the cut are. For a few cuts a day, a piston compressor such as the E 75, followed by a dryer, is suitable. For daily cutting, the K 75 4-in-1 screw compressor supplies dry air straight from the unit. See our article on the compressor for a 45 A plasma cutter.
Which compressor for a 125 A CNC plasma table?
A 125 A power source needs, as a guide, around 250 to 280 l/min at the torch at 6 to 8 bar, plus the table's auxiliaries. With a margin, plan on about 0.5 m³/min per table. The K 75 (1.1 m³/min at 8 bar) supplies one table; the K 110 (1.7 m³/min at 8 bar) takes over for two tables or to keep a reserve. A table cuts for hours on end: that is continuous duty, which is what a screw compressor is built for.
How can I check that the air reaching the plasma torch is dry enough?
After a long cutting session, drain the bowl of the power source filter, disconnect the air supply at its inlet and blow for a few seconds onto a clean, dry cloth or a cold mirror. Traces of moisture or oil show that the air treatment is not enough. Run this test at the power source inlet, not at the compressor outlet: what counts is the air that reaches the torch.
The recommended models
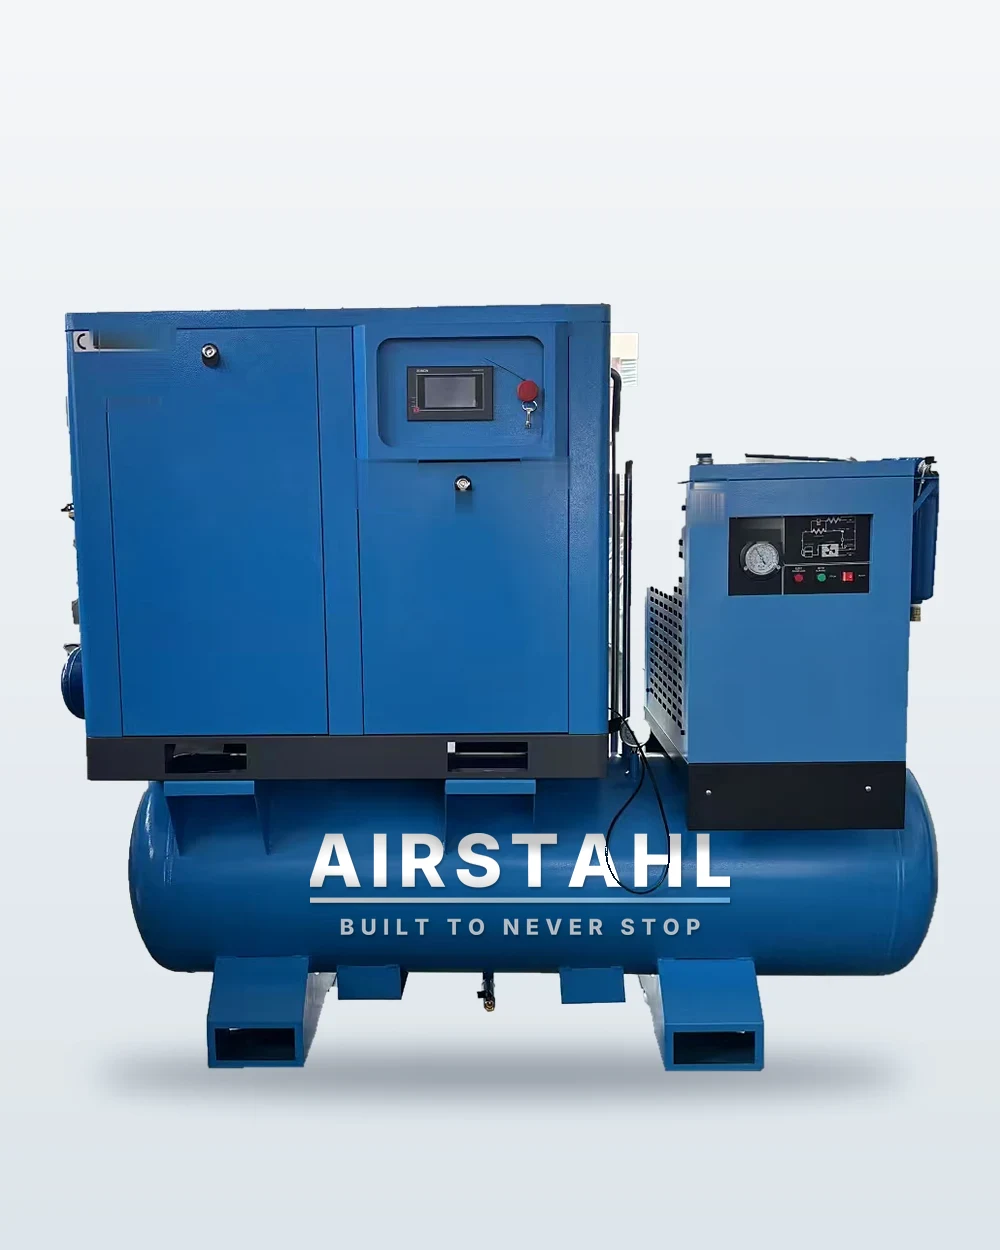 7.5kW
K 75Screw compressor 7.5 kW 4-in-1
Compressor, 420 L air receiver, refrigerated dryer and filtration combined on a single frame.
11kW
K 110Screw compressor 11 kW 4-in-1
Compressor, air receiver, refrigerated dryer and filtration combined on a single frame, at 11 kW.
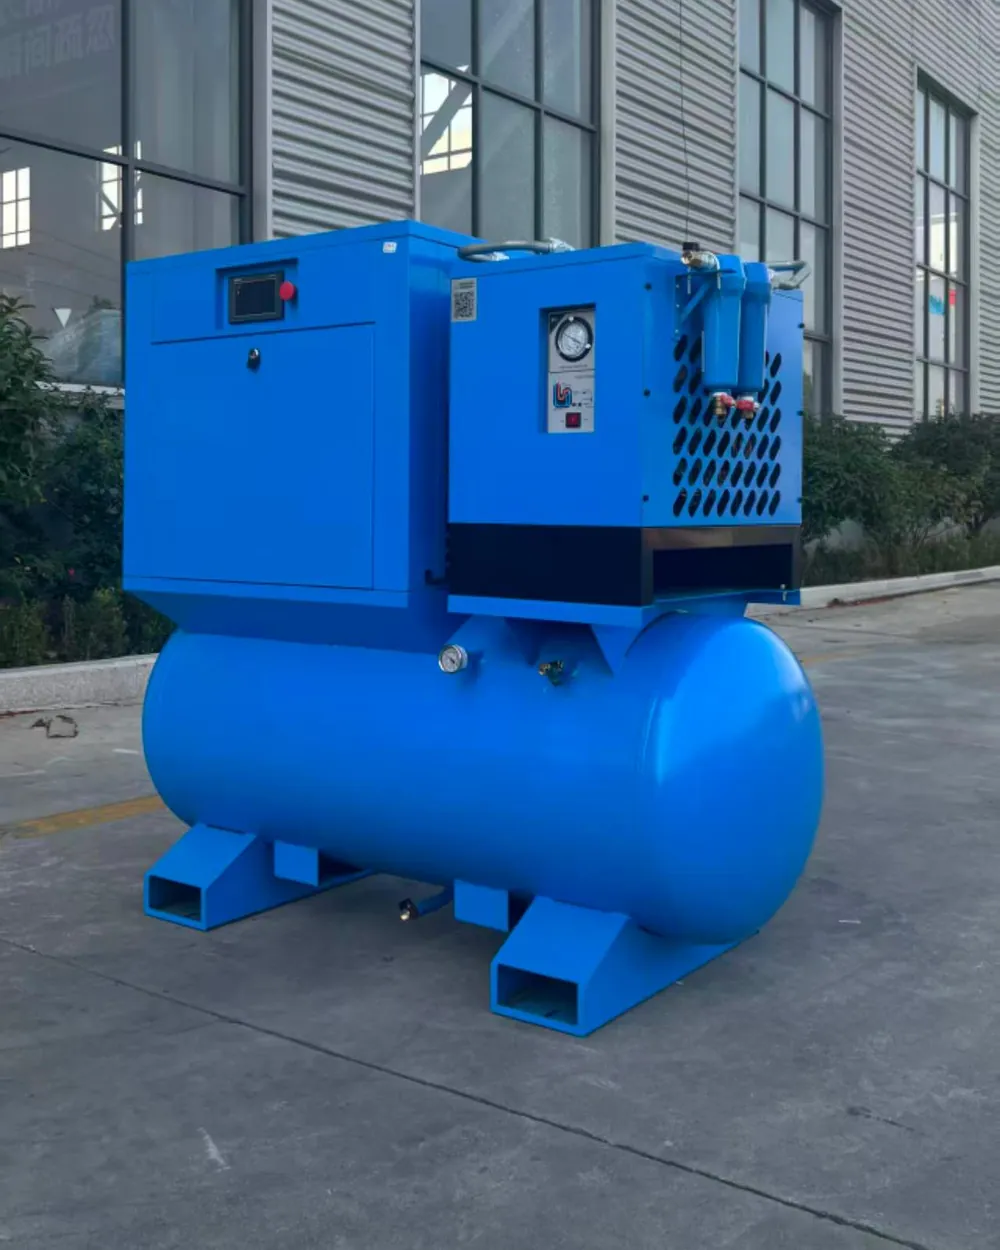 15kW
K 150Screw compressor 15 kW 4-in-1
Compressor, air receiver, refrigerated dryer and filtration combined on a single frame, at 15 kW.
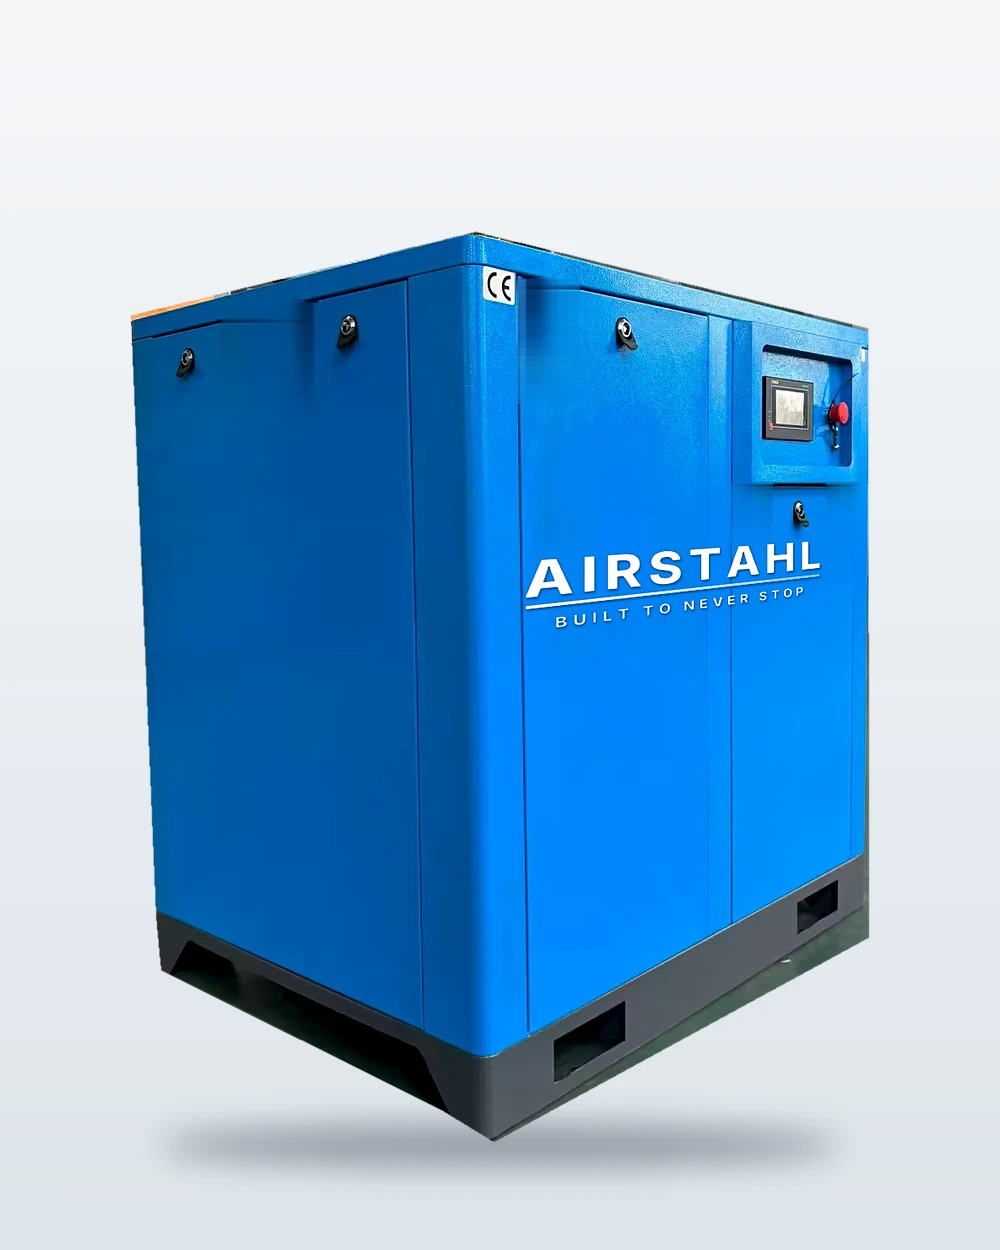 15kW
S 150Screw compressor 15 kW
For production workshops and truck workshops with high air consumption.
Other trades
A project, a question?
We answer quickly and quotes are free. Tell us what you run on air and we'll point you to the right model.